01Observe the real work before the paperwork
Compare standard procedures with actual setup, inspection, and exception handling.
Capture conditions, signals, decisions, actions, and outcomes rather than producing a simplistic answer book.
Observation is required because the shop floor itself is thinning. According to Japan's 2026 White Paper on Manufacturing Industries (METI, MHLW and MEXT, approved by Cabinet on 29 May 2026), the share of manufacturers using digital technology rose from just under 50% in 2019 to over 80% in 2024. Over roughly the same two decades, employment in manufacturing fell by 1.57 million. Holding on to the judgement criteria that live in experienced workers' heads is getting harder as an organisational matter.
Start by filling in the observation sheet below, one event per row. The last column, whether the step appears in the standard procedure, turns the gap between documents and practice into a list. Processes with many "no" rows are the first candidates for knowledge cards.
If you are unsure where to start, run a process inventory first. Good candidates are processes that generate many questions to experienced staff, or changeovers where the steps vary from day to day.
| date | process | equipment | operator | conditions (material | temperature | preceding job) | signals (sound | readings | appearance) | decision (what was checked and what was decided) | action | outcome | in standard procedure? (yes/no) |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
02Make tacit knowledge verifiable
Structure knowledge by equipment, product, process, symptom, possible cause, and verification method.
Attach source, date, and approver. When evidence is insufficient, the assistant should escalate rather than improvise.
Use the knowledge card below as the container. Keep one symptom per card. Both "first response" and "escalation trigger" must be filled in, and a card with either field empty is not approved. If the card does not say how far the operator may act alone, the assistant cannot say it either.
The approver should be the role accountable for quality or equipment in that process. The experienced operator supplies the content but is not the approver. A next review date stops outdated knowledge from staying in use after a material or machine change.
# Knowledge card No. ___
| Field | Entry |
|---|---|
| Equipment | |
| Product / part number | |
| Process | |
| Symptom (what the floor can see) | |
| Possible causes (most likely first) | |
| How to check (who, with what, where) | |
| First response (what the operator may do) | |
| Escalation trigger (when to call the owner) | |
| Final decision owner (quality and safety) | |
| Source (observation No., interview date, procedure) | |
| Approved by / date | |
| Next review date |
03Worked example: first-article check after a mould change
The following is a fictional example. It shows the first response to a defective first article after a mould change in injection moulding, written up as a knowledge card. Machine names, part numbers and dates are illustrative only and do not come from any real plant.
Note two things. The possible causes are ranked, and the operator's scope stops at waiting and taking another sample. The card does not tell the operator to change process conditions, because that affects quality and belongs to the team lead beyond the escalation trigger.
The source field points back to an observation record and an interview date. Only cards that trace back to an observation record go into the assistant's reference set. A card based on interview alone is approved after the event has been observed the next time it happens.
# Knowledge card No. 012 (fictional example)
| Field | Entry |
|---|---|
| Equipment | Injection moulding machine No. 3 |
| Product / part number | Resin cover A-100 (example) |
| Process | First-article check after a mould change |
| Symptom (what the floor can see) | Short shot on the flange of the first article (resin does not fill) |
| Possible causes (most likely first) | 1. Material not dried enough 2. Mould not yet at temperature 3. Blocked gate |
| How to check (who, with what, where) | Operator checks dryer setting and elapsed time on the log sheet, and mould temperature on the controller display |
| First response (what the operator may do) | Wait until drying time and mould temperature are within the condition sheet, then take a new first article |
| Escalation trigger (when to call the owner) | Two consecutive short shots with conditions in range, or visible debris near the gate |
| Final decision owner (quality and safety) | First-article disposition: QA team lead. Machine stop: production manager |
| Source (observation No., interview date, procedure) | Observation No. 034, interview with experienced operator (e.g. Sep 2026), moulding condition sheet rev. 3 |
| Approved by / date | Production manager (e.g. Sep 2026) |
| Next review date | e.g. Mar 2027 |
04Separate assistance from quality decisions
Search, checklists, and record formatting are suitable early support cases.
Product disposition, equipment shutdown, and safety decisions remain with named owners and explicit standards.
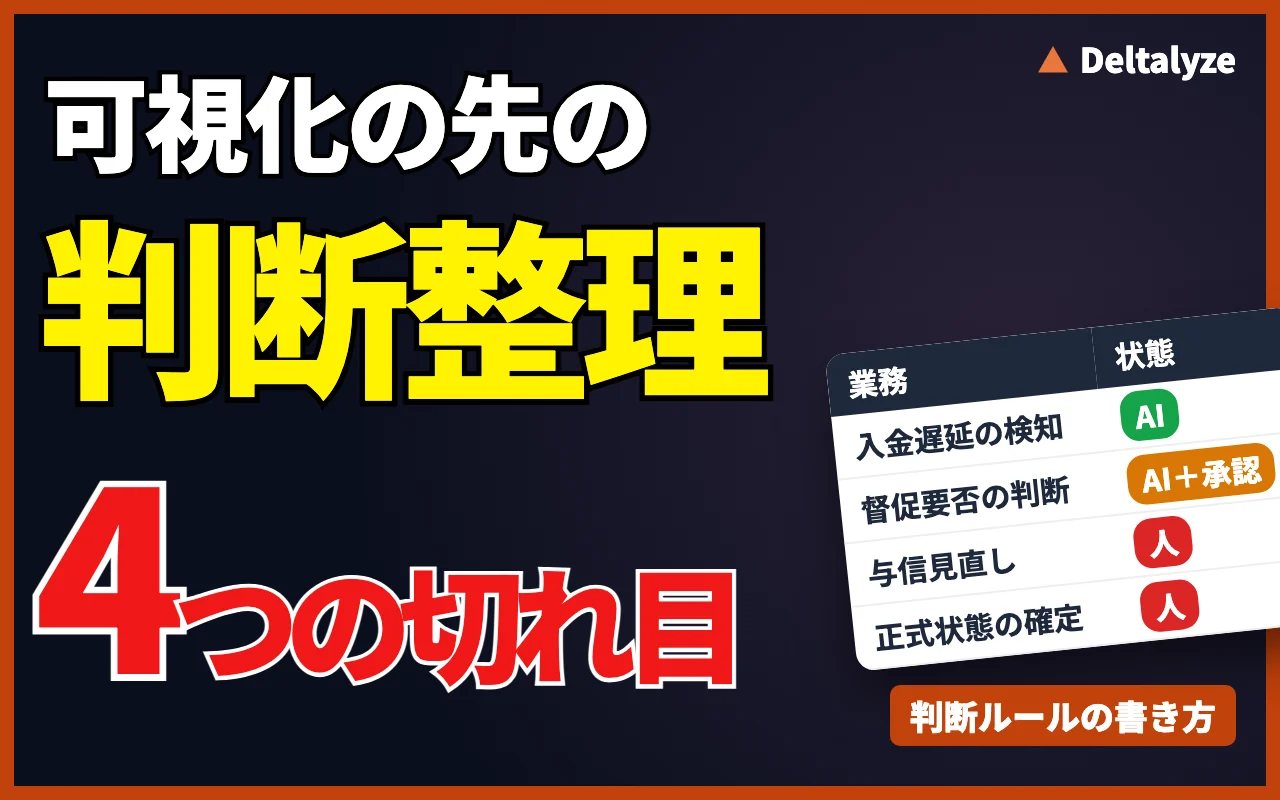
Draw the line with the decision table below. "What AI may do" stops at gathering and arranging inputs. Rows for disposition and stopping say "not delegated", and the assistant may only point to the criteria and the owner. Write owners as roles, not personal names.
Back-office functions need the same line. For the internal-control view, see control checkpoints before using AI in accounting.
Once the table is agreed, write the same boundaries into the assistant's instructions. The prompt below uses approved cards as the only source and escalates instead of answering when evidence is missing. Recording why a suggestion was not used reveals operational problems that model accuracy alone does not show.
| Task | What AI may do | Decision kept by people | Example owner |
|---|---|---|---|
| Search procedures and past records | Find and show matching cards and records | Whether to use the procedure | Operator |
| Present inspection items | List checks for the symptom, in order | Reading the check results | Operator |
| Format work records | Turn spoken notes into the record format | Confirming the record | Shift lead |
| Suggest possible causes | Show causes from cards, with sources | Identifying the cause | Maintenance |
| Product disposition | Not delegated (organise inputs only) | Accept, reject, hold | Quality assurance |
| Stopping or restarting equipment | Not delegated (show stop criteria only) | Stop and restart | Production manager |
| Safety-related actions | Not delegated (point to the procedure only) | Whether work may proceed | Safety manager |
You are a work-support assistant for a manufacturing floor. Follow these rules.

# Allowed information
- Base every answer only on the "knowledge cards" and "work records" pasted below.
- Do not fill gaps with general knowledge or guesses.

# How to answer
1. State the number of the knowledge card that matches the symptom the operator entered.
2. List that card's "how to check" and "first response" steps in order.
3. After each step, add the card or record number you relied on in brackets.
4. If an "escalation trigger" applies, start with "Contact the owner now" and name the role to contact.

# Do not answer
- Do not answer product disposition, stopping or restarting equipment, or safety decisions. Escalate to the role listed as "final decision owner".
- If no card matches, reply only: "No matching knowledge. Please check with the owner."

# Knowledge cards
(paste here)

# Operator input
(describe the symptom here)
Paste approved cards only. If an answer has no source number, do not use it and check with the owner.
05Run a controlled parallel pilot
Compare the assisted process with the current process in one bounded operation.
Measure response time, recurrence, record completeness, and expert interruptions while protecting safety and quality thresholds.
Fix the measures before the pilot and record the baseline the same way. Choosing measures afterwards leaves only the flattering ones. During the pilot, log in one line whether each suggestion was used and, if not, why.
Decide on expansion by looking at whether escalation happened when it should have, not only at the measures. If the assistant answered where it should have escalated, fix the cards and the prompt before extending to similar equipment or adjacent processes.
- Pick one process
Choose one with many undocumented rows and frequent questions to experienced staff. Do not start with a process directly tied to safety.
- Record the baseline
Capture downtime, first-response time, recurrence, missing records and questions to experienced staff, using the same method you will use afterwards.
- Approve knowledge cards
Write cards for the most frequent symptoms first. Only approved cards go into the assistant's reference set.
- Run side by side
Operators keep following the current procedure and use the assistant as a check. Log adoption, rejection and the reason.
- Review escalations
Each week, check whether escalation happened when required and whether any answer lacked a source. Fix cards and prompt.
- Decide on expansion
The approver reviews the measures and the escalation log and decides whether to extend to similar equipment or adjacent processes.
06Create reusable plant-level building blocks
Separate shared procedures from site-specific exceptions.
In card terms, keep symptom, possible causes and checks in a shared card, and put condition values and contact roles in a site-specific appendix. When a shared card changes, you can then see which sites' appendices need checking.
Version knowledge, workflows, and permissions together so teams can see the impact of every change. For the conditions that let the floor lead this work, see operator-led AX.
KEY TAKEAWAYS
What to carry into implementation
- List the gap between real work and standard procedures with an observation sheet
- Give every knowledge card a source, review date, approver and escalation trigger
- Separate assistance from quality and safety decisions with a decision table
- Pilot in one process and check measures and escalations before scaling
FAQ
Frequently asked questions
Is the goal to replace experienced operators?
No. The goal is to reduce search and recording burden, preserve expert judgment, and make validated knowledge reusable.
How should results be measured?
Use operational measures such as response time, recurrence, record quality, and expert interruptions while keeping safety and quality as hard gates.
How many knowledge cards do we need to start?
Coverage of the most frequent symptoms matters more than the count. Once the main symptoms of one process are covered, the pilot can start. Add cards for whatever triggered escalations during the pilot.
What if experienced staff have no time to explain?
Observe first and fill in the observation sheet, then ask them only to review and add to the records. Answering against a record takes far less of their time than explaining from scratch.
What happens if the assistant shows a wrong procedure?
Every answer carries a card number, so the faulty card can be traced, reviewed and re-approved before it returns to the reference set. Disposition and stop decisions were never delegated, so an error does not become one of those decisions directly.